Solar Panel Manufacturing Process: 10 Steps and Machines
Table of Contents
Quick answer: Solar panel manufacturing runs as a continuous process timed by takt, not as ten independent machines. A box of graded cells enters, and a palletized, tested module leaves, through cell testing, cutting, stringing, layup, lamination, trimming, framing, junction-box fitting, curing and final IV testing. Throughput is set by the slowest station, so a line is specified by annual capacity — a 120 MW line and a 20 MW line use the same sequence at different station counts and speeds. Ribbon placement and soldering at the stringer, and the vacuum and thermal profile at the laminator, are where most defects originate; two electroluminescence gates catch micro-cracks and voids before they reach a customer. The same process serves PERC, TOPCon and back-contact cells, with cell format and busbar count as the main variables.
What actually happens between a box of incoming cells and a palletized module — every step with its machine, cycle time, power draw, floor space and operator count, from a supplier whose lines run this process daily.
PV Module Production · Process & Equipment Guide · by Jerry, Ooitech
A 120 MW automatic line finishes a module roughly every two minutes. Ten steps stand between a box of incoming cells and that palletized module, and each step has a machine, a cycle time, a price and a failure mode. Most descriptions of the solar panel manufacturing process stop at the science. This page walks it the way you would audit it on a factory floor — because that is the version you need before signing an equipment contract.
1. How the Process Actually Runs: Takt, Not Ten Separate Machines
The word that governs everything is takt — the rhythm at which finished modules leave the line. On our 20 MW semi-automatic configuration the line completes 16 panels per hour; on the 120 MW automatic line, 32 panels per hour running 24 hours a day. Every station upstream must keep pace with that rhythm or become a bottleneck, and the two slowest operations — soldering and lamination — set the tempo for everything else.
That is also why the process list below reads like a quotation sheet. Each of the ten steps maps to one machine group with a fairly stable market price band, FOB China: entry-class stringers sit in the $60k–70k range, the workhorse 2,400-cell class between $99,000–120,000 and $140,000–150,000, a laser scribing machine around $20k–25k, a turning unit a few thousand dollars — bands that have moved surprisingly little across several years of quoting. When you finish this page you should be able to look at any supplier's process diagram and attach a price band and a labor count to each box in it.
2. The Ten Steps, From Cell Testing to Pallet
| Step | What happens | Machine (typical FOB China band) | Key number |
|---|---|---|---|
| 1. Cell testing | Incoming cells flash-tested and binned by Isc, Voc, Pmax, FF, Rs, Rsh | Cell tester, OTCT-A class ($15k–18k) | 10 ms flash · cells up to 210×210 mm |
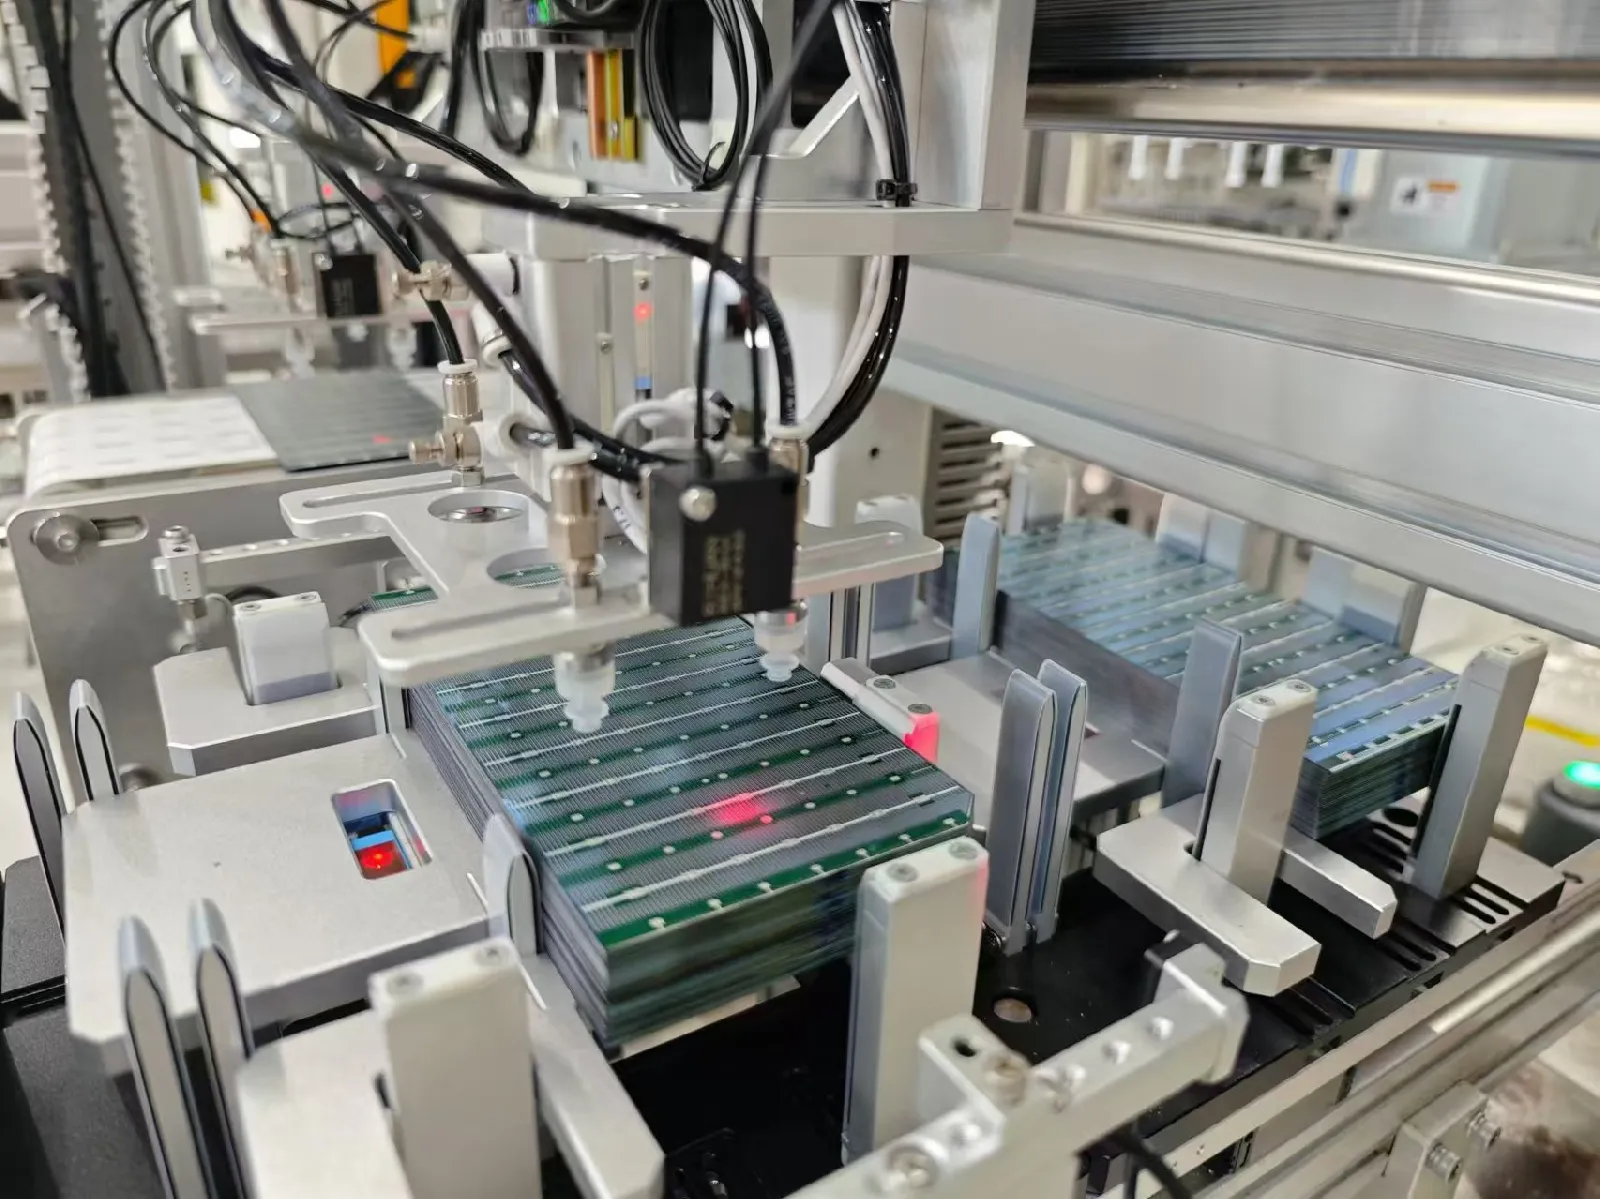
| 2. Laser scribing & splitting | Full cells scribed then split into half or quarter cells | Laser scribing, OLS-20A class ($20k–25k) | 1,500 full cells/h · 40 μm scribe · breakage ≤0.3% on A-grade |
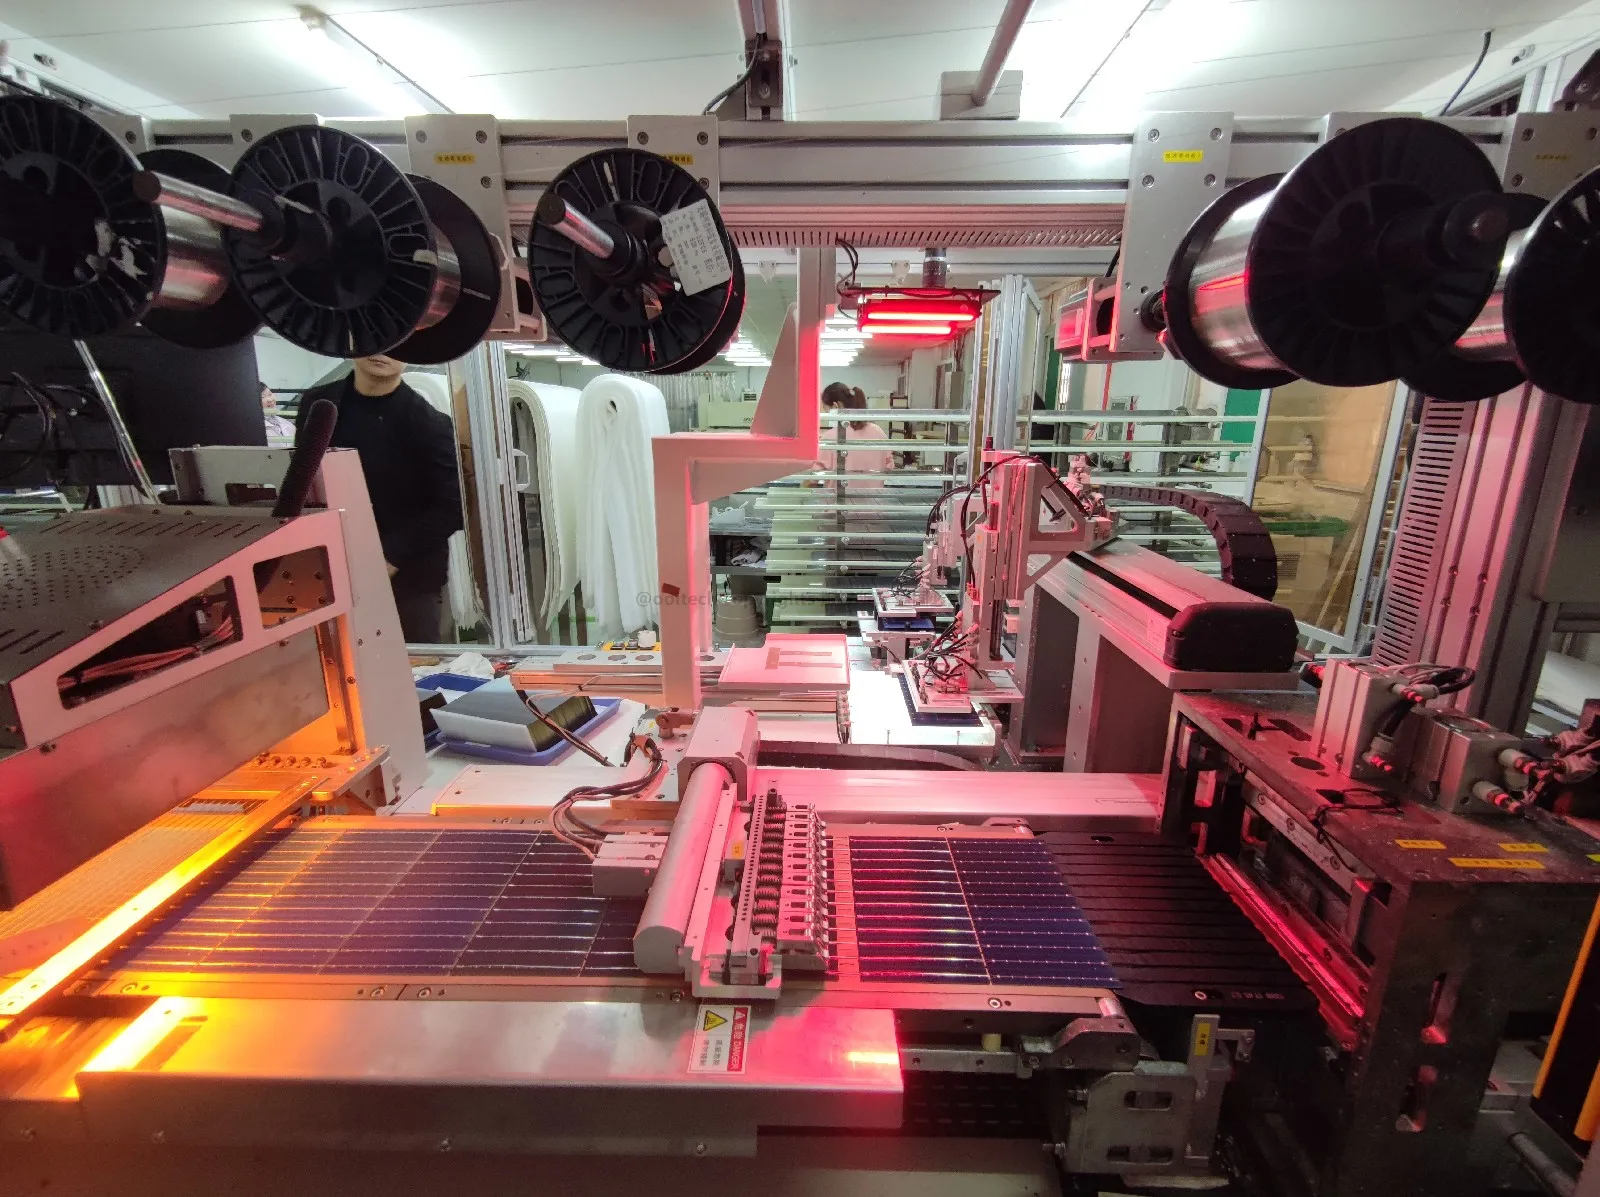
| 3. Tabbing & stringing | Ribbon soldered front-to-back, cell to cell, into strings | SS-1500 class ($60k–70k) / SS-2500 class ($120k–140k); ATW class ($380k–430k) | 2,400 cells/h (SS-2500) · IR soldering · breakage ≤0.2% |
| 4. Layup | Glass, EVA, strings, second EVA layer and backsheet stacked in order | Glass loader $25k–30k · auto layup $50k–60k · EVA/TPT cutter $8k–35k · manual layup stations from ~$1,400–1,700 | Semi-auto: 4 stations for 16 panels/h |
| 5. Bussing | Strings interconnected into the full circuit; j-box ribbon laid | Manual bussing tables ($4k–5k) or automatic bussing ($130k–260k) | The biggest single scope swing between quotes |
| 6. Pre-lamination EL | Electroluminescence imaging catches microcracks and misaligned ribbons | EL tester, 8-camera class ($25k–32k) | Last chance before the irreversible step |
| 7. Lamination | Stack melted under vacuum and heat into one bonded laminate | OCY-2666 class ($90k–105k) single-chamber; double-chamber $150k–200k | 98 kW rated · 40 Pa vacuum · ±1–2 °C uniformity |
| 8. Trimming & framing | Edge flash removed, aluminum frame glued and pressed | Manual trim $4k–5k / auto $30k–35k · framing $6k–8k semi / $45k–52k auto / $140k–185k all-in-one | All-in-one adds glue-flow control |
| 9. Junction box & curing | J-box glued, wired, potted; adhesive cures on a conveyor | Gluing $5k–6k · potting $12k–17k · auto welding $60k–70k · curing conveyor $30k–70k | 2 operators on our 150 MW staffing plan |
| 10. IV & final EL test, packing | Sun-simulator flash assigns the power class; final EL verifies no new cracks; module packed | IV tester, OTMT-A class ($20k–28k) or Gsolar Class A ($60k–75k) · final EL 4-camera ($20k–23k) | 10 ms flash · modules to 2500×1400 mm |
Four of those steps decide most of your economics, so they deserve a closer look.

Step 3 — stringing, the irreversible one
Soldering ribbon to a cell's front face and routing it to the next cell's back is where a module's electrical quality is locked in. The SS-2500 does it at 2,400 cells per hour with CCD camera positioning and a robot handling each cell, holding breakage at or below 0.2% on A-grade cells across 3–20 busbar formats from 156 to 210 mm. Once a bad solder joint or a hidden microcrack passes this station, no later step can repair it — which is why step 6 exists. When something drifts, the symptom is specific: wires sitting off their solder pads, visible as blackened or unwetted joints at the string edge. The fix is nearly always ribbon feed alignment or the soldering temperature recipe, not the cell.
Step 7 — lamination, the tempo-setter
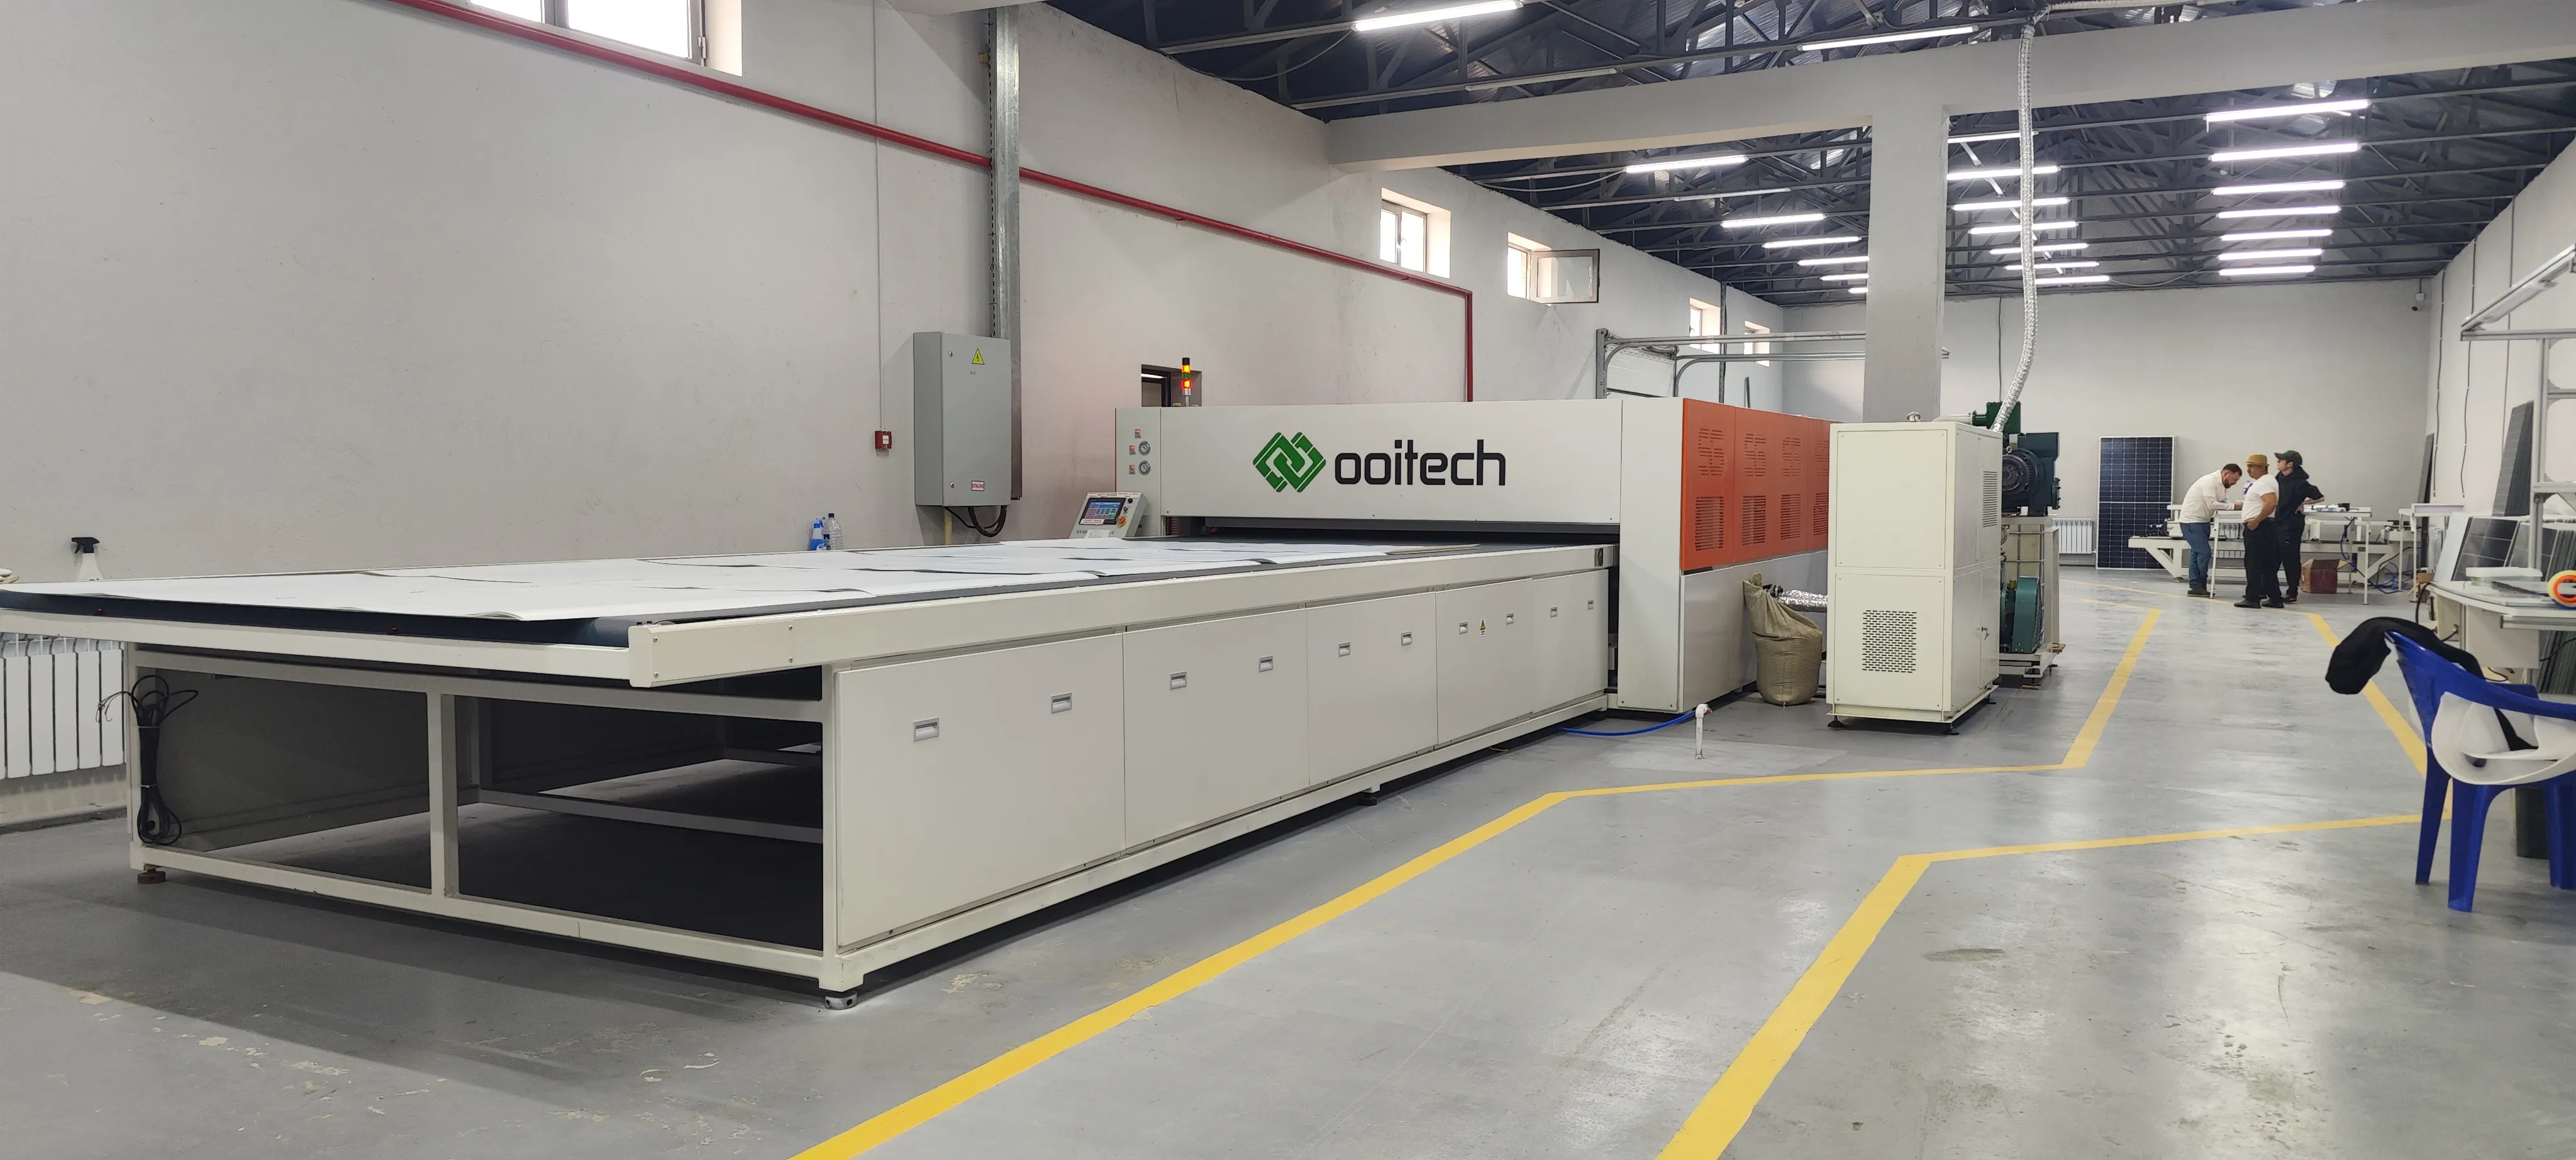
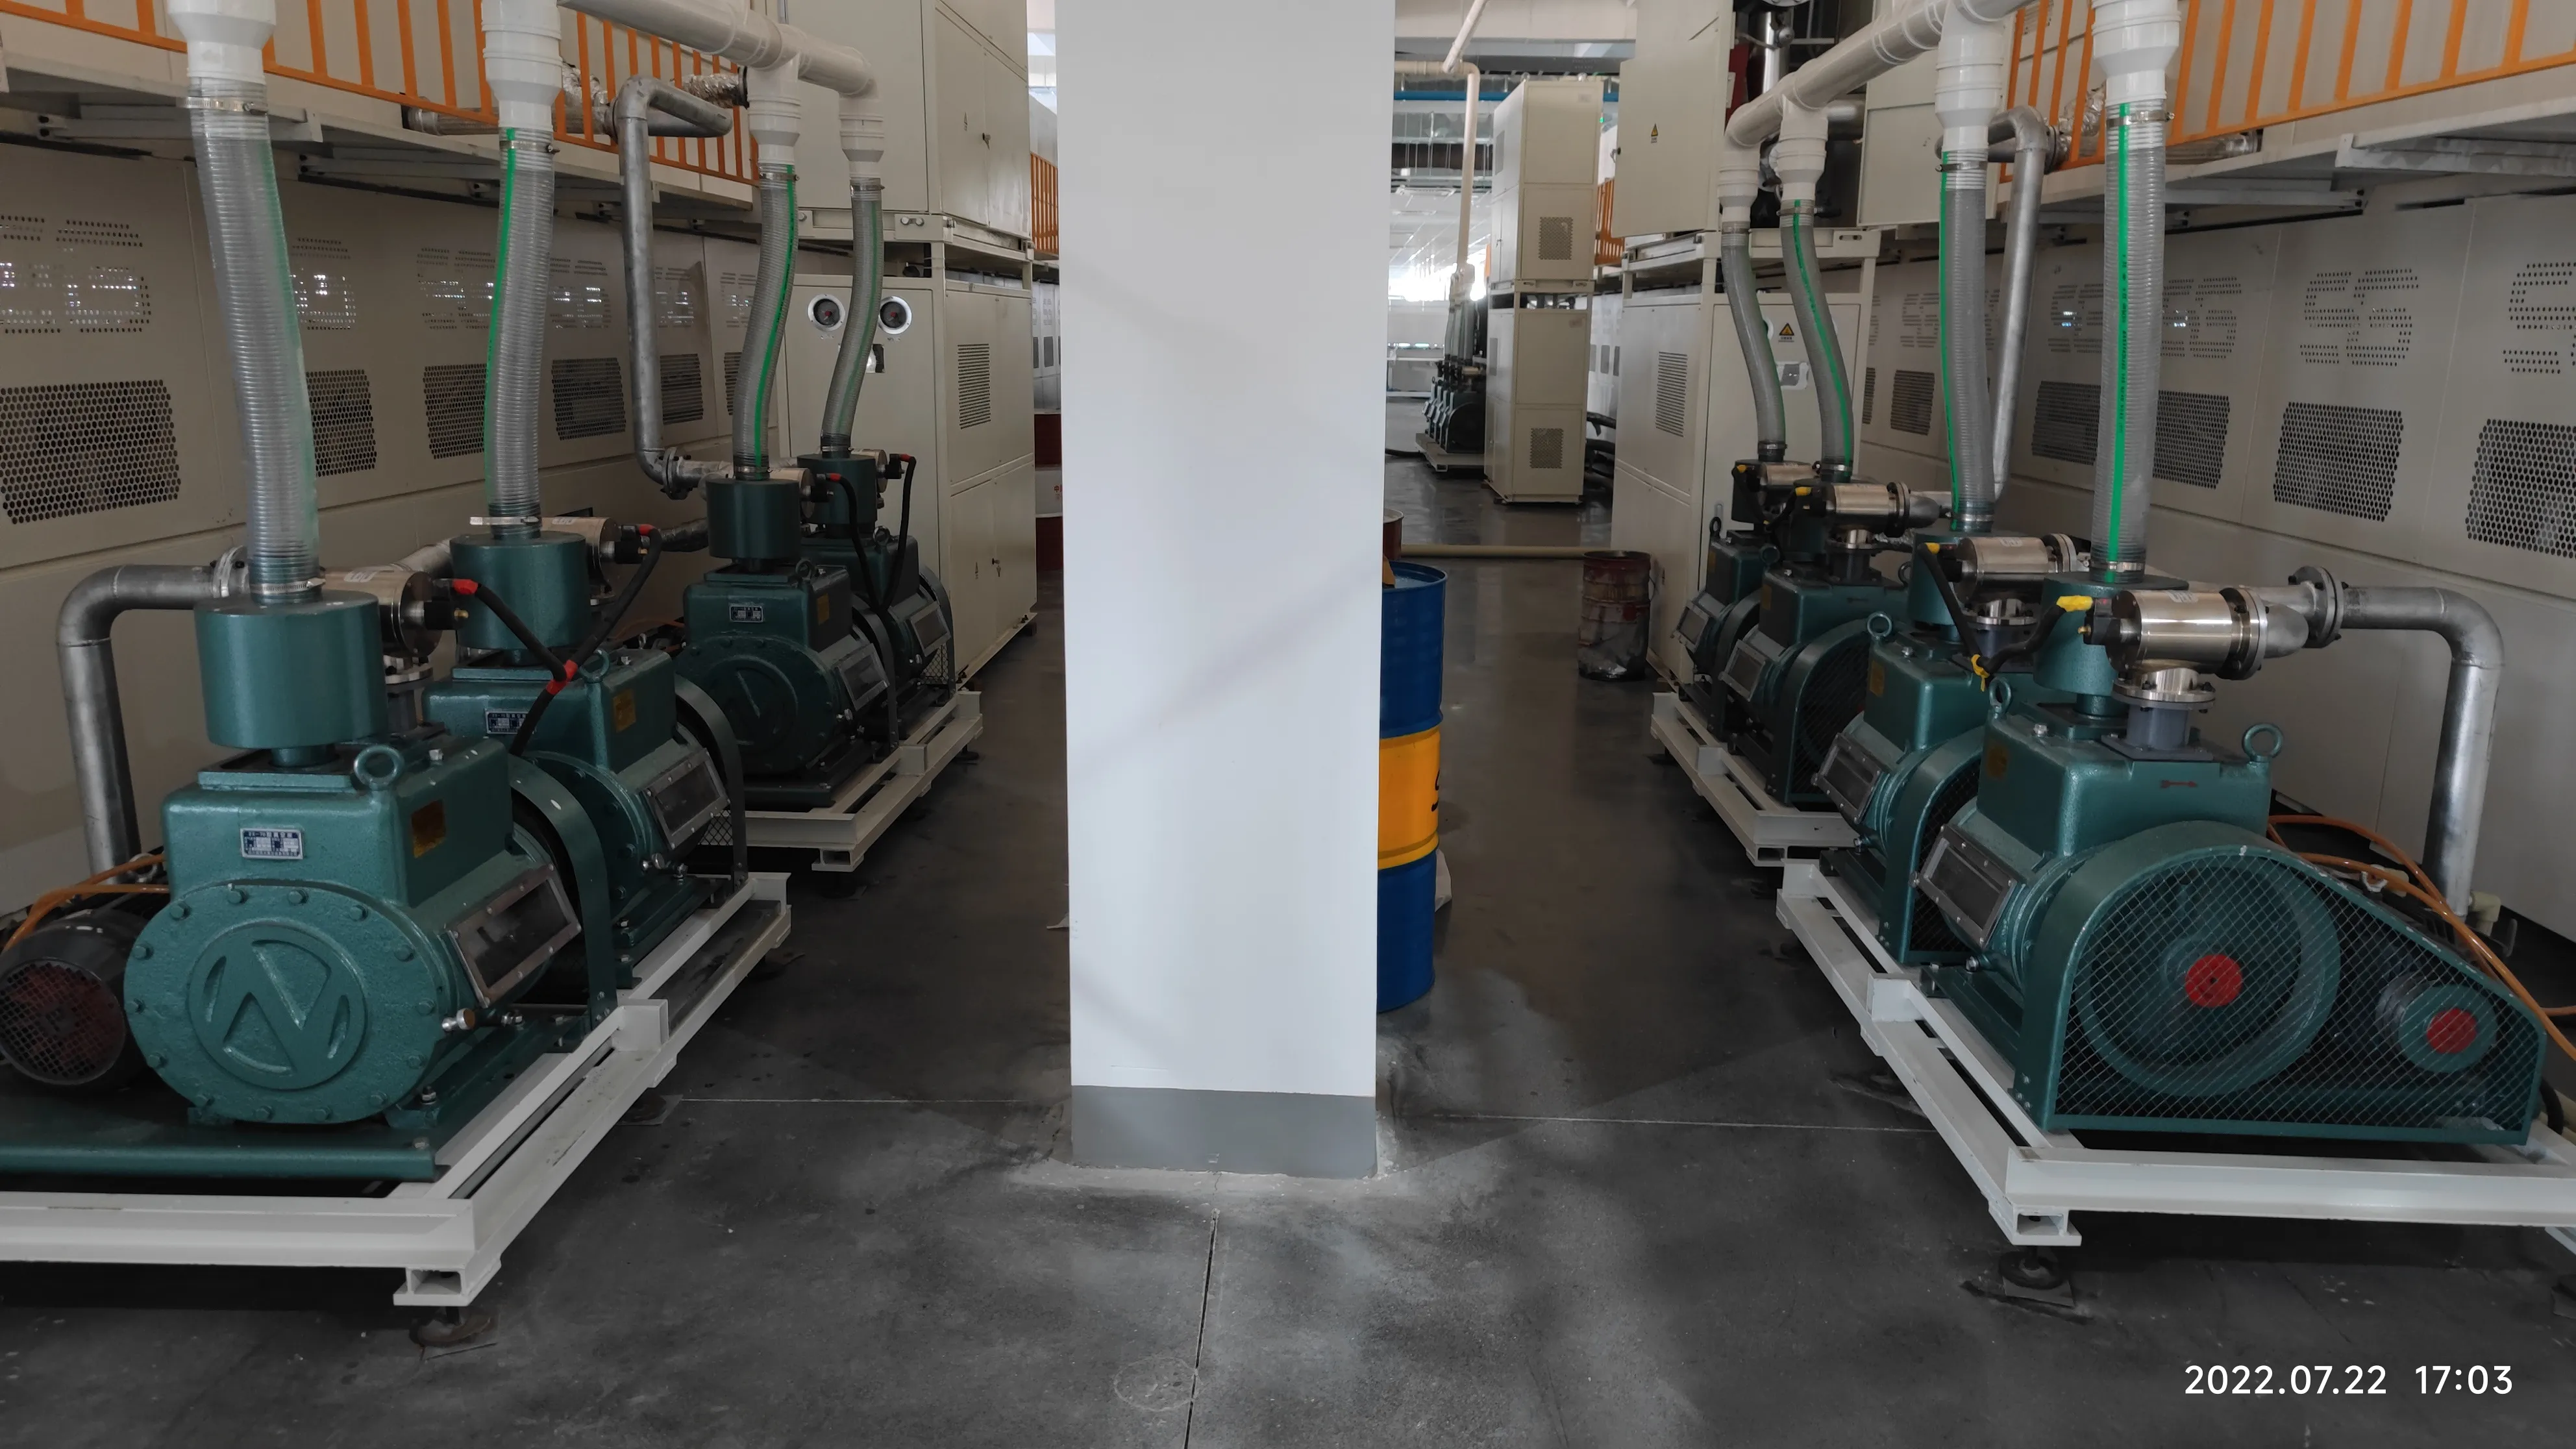
The laminator is the one machine every module must sit inside. The OCY-2666 class offers a 2600 × 6600 mm work surface, oil heating with temperature uniformity held to ±1–2 °C, vacuum down to 40 Pa and pump-down cycles of 5–30 minutes — which is why lamination, not soldering, sets line takt on smaller lines. It is also the hungriest single machine electrically: 98 kW rated, 72 kW of that heating. At the 120 MW tier the sheet typically moves to a double-chamber machine ($150k–200k) so one chamber cures while the other pumps down; at 300–600 MW, double-chamber double-layer units running into the $400k range each.
Steps 4, 5 and 8 — where semi-automatic saves and costs
Layup, bussing and trimming are the three steps that exist in both a $1,400–1,700-class manual station version and a $45,000–290,000 automatic version. The solar panel production process is chemically identical either way; what changes is who does the work. A semi-automatic 20 MW line puts four operators at layup tables, two at bussing tables, one at trimming — and the whole line lands in the low-to-mid $300k range. The automatic equivalents delete those positions and add conveyors, turning units and centering stations instead. Neither is "better": where operator wages run $400–700 a month the manual version pays back, and where they run at European levels the automatic one is the only sensible configuration.
Steps 1, 6 and 10 — the quality gates
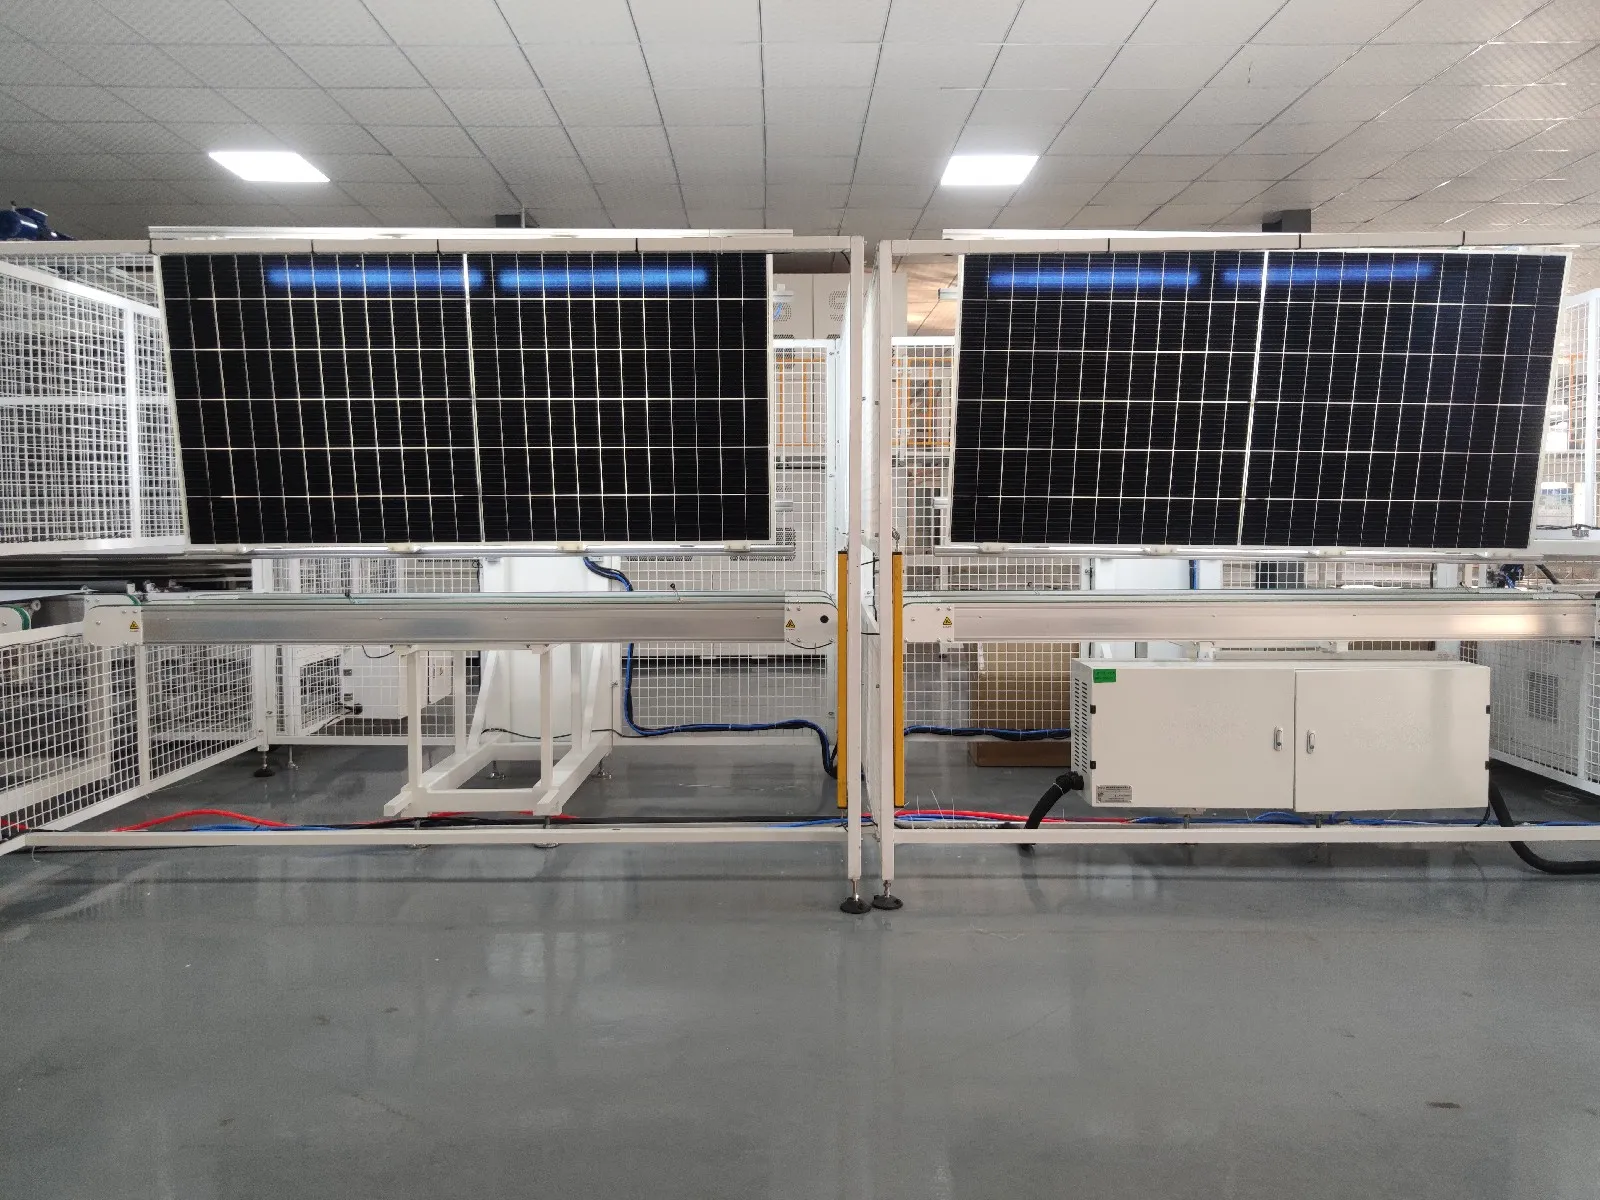
Three of the ten steps test rather than transform, and together they cost somewhere in the $60k–100k band of equipment: cell tester, pre-lamination EL, IV simulator and final EL. Buyers stretching a budget are tempted to cut one. Don't. Without incoming cell binning you mix grades in one string; without pre-lam EL you laminate cracks shut and find them after the most expensive step; without a final IV flash you ship power classes you never measured. The gates are the cheapest machines in the factory relative to the losses they prevent.

3. What the Process Consumes: Space, Power, Air, People
Serious buyers send us a checklist that reads almost identically every time: production capacity per machine, cycle time, power requirement, air consumption, operators required, machine dimensions, automation level. Here is that checklist answered for the three standard tiers, from our own quotation sheets and factory layout drawings.
| Resource | 20 MW semi-auto | 60 MW automatic | 120 MW automatic |
|---|---|---|---|
| Output rhythm | 16 panels/h, one 8 h shift | ~24 panels/h class | 32 panels/h, 24 h operation |
| Production hall | ~600–800 m² class | ~800–1,000 m² class | ~1,000 m² (50×20 m) |
| Warehouse (cells in / modules out) | roughly the same area again, all tiers | — | — |
| Ceiling / doors / columns | Ceiling 4.2–6 m · doors 5–6 m wide · column-free preferred, otherwise spacing ≥6 m (from the 120 MW layout sheet) | ||
| Installed power | ~150–200 kW class | ~350–500 kW class | ~700 kW |
| Compressed air | Thousands of liters per minute at the automatic tiers — sized per layout; pneumatic cylinders run framing, turning units and loaders | ||
| Operators per shift | Semi adds manual layup, bussing, trimming positions | Lean automatic crew | 12–15 operators + 2 engineers; 24/shift on the 150 MW double-glass plan |
| Hall environment | Stringing and lamination zones want 25 °C ±2 and 50–60% RH — a warehouse conversion usually pays for climate control retrofit | ||
On staffing, the 150 MW double-glass staffing plan is worth reading station by station, because it shows where the people actually go: one operator at the stringer, one each at glass feeding, EVA feeding, spacer placement and busbar/tape feeding, one at pre-lamination EL, three in rework, one each at edge taping, trimming, flip inspection and glue/frame, two at the junction-box station, one fitting box covers and cleaning the rear, one cleaning the front, one swapping IV/EL test fixtures, one each at IV and final EL, two applying nameplates and barcodes, two unloading. Twenty-four people, and not one of them is optional on a double-glass line at that automation level — rework alone carries three, because step 6 and step 10 keep feeding it.
4. Where Defects Are Born — and the Two EL Gates
Every experienced process engineer in this industry says the same thing about yield: defects are cheap to catch before lamination and expensive after it. The pre-lamination EL gate at step 6 exists because stringing is irreversible; the final gate at step 10 exists because lamination itself, framing, and handling can all introduce new cracks after the first gate has passed. Between them, the two EL stations cost well under $54,000–66,000 combined and catch the failure modes that otherwise surface as year-three warranty claims: microcracks under the ribbon, cold solder joints, and cells cracked in transport through the line.
The practical question to ask any supplier is what happens between the two gates when a defect is found. Rework before lamination means re-laying a string — minutes. After lamination it means scrapping a bonded laminate that already contains its glass, EVA, cells and backsheet: at roughly $55–60 of materials per 585 W-class module, three escaped defects a day is a five-figure annual materials loss that never appears in an equipment quotation.
5. One Process, Three Technology Routes
The ten steps do not change when the cell does — but two machines in the list have to be told what they are feeding. An SS-2500 stringer covers PERC and TOPCon in 3–20BB formats natively; HJT's low-temperature requirements and back-contact (BC) formats need a compatible stringer configuration, which is why buyers planning BC or HJT volume should confirm stringer compatibility before anything else on the sheet. Buyers also ask us, correctly, whether one line can run several cell types at once for tolling work — the answer is yes with quick-change cell kits and a re-validated soldering recipe per format, at the cost of changeover time. What the process never tolerates is mixing grades within a string: step 1's binning exists precisely so that matched cells enter step 3 together.
FAQ — Solar Panel Manufacturing Process
How long does one solar panel take to make?
Line output is measured in takt, not per-panel time: a 120 MW automatic line finishes a module roughly every two minutes, a 20 MW semi-automatic line every three to four. But any single module spends longest inside the laminator — pump-down and curing run 5–30 minutes per cycle — which is why larger lines use double-chamber machines to overlap cycles.
How many workers does a solar panel production line need?
On our 150 MW double-glass staffing plan, 24 operators per shift plus line engineers; the 120 MW automatic sheet specifies 12–15 operators plus 2 engineers; semi-automatic tiers add manual positions at layup, bussing and trimming instead of paying for the automatic machines. The staffing count follows the automation scope, not the capacity number.
How much floor space does the process need?
About 1,000 m² of production hall for a 120 MW line (50×20 m, 4.2–6 m ceiling, doors 5–6 m wide, columns at 6 m or more), plus roughly the same area again for raw-material and finished-module warehousing. A 2,000 m² hall therefore fits a 50–100 MW line with a workable but tight warehouse; smaller lines scale down from there. Second-floor placements work only for the lighter stations — lamination's floor loading and the layout's straight-line flow usually anchor the heavy end at grade.
How much electricity does a solar panel factory consume?
Plan for roughly 700 kW installed at the 120 MW automatic tier, with the laminator (98 kW rated on the 2666 class) and the IR stringer as the two largest draws. Average consumption runs well below installed capacity and scales sub-linearly: published industry figures put a 30 MW line near 150 kW average and a 400 MW line near 360 kW.
Can one production line run PERC, TOPCon and BC cells?
PERC and TOPCon run on the same SS-2500-class stringer (3–20BB, 156–210 mm). HJT and back-contact formats need a low-temperature or BC-compatible stringer configuration — confirm this before quoting anything else. The other eight steps are cell-type agnostic apart from recipe settings and test fixtures.
Which step causes most defects?
Stringing. It applies heat to a 130–180 μm wafer and it is irreversible: ribbon misalignment off the solder pads, cold joints and microcracks all originate there. That is why breakage specs (≤0.2% on A-grade cells for the SS-2500) and the pre-lamination EL gate matter more than any throughput figure on the sheet.
What raw materials does the process consume?
Per 585 W TOPCon module, roughly $55–60 of materials at mid-2025 market prices: cells alone over 40% of the bill, frame and tempered glass together around 30%, then solder strip, backsheet, POE, EVA, junction boxes and sealant. A 120 MW line consumes that continuously at 32 panels per hour, paid largely in advance as a first-year buyer — the working-capital number that decides whether the process keeps running.
Is training really needed if the machines are automatic?
Yes. The machines run themselves; the process does not. Operators need two to three months to hold rated yield — recipe changes per cell format, EL image reading, ribbon and cutter alignment checks are human skills. Our standard scope includes 30 days of on-site commissioning and training plus lifetime remote process support, because most yield problems after month one are recipe and alignment questions, not hardware failures.
Specifications reference Ooitech machine data; price bands reflect typical FOB China market ranges per machine class and move with configuration and exchange rates — confirm a current quotation before budgeting.
Related reading: how machine prices are built, plant cost, utilities and staffing, and how to start a solar panel manufacturing business.
What machines and equipment are required for solar panel manufacturing for commercial purposes?
For commercial module production the core list is: a cell tester and sorter, a tabber and stringer, a layup station, a bussing or auto-bussing machine, an EL tester after stringing, a lamination stacker, a laminator, a trimming machine, a framing machine, a junction-box and potting station, a curing oven, a second EL tester, an IV tester with a sun simulator, a hipot and insulation tester, and a cleaning and packing area.
Around that core sit supporting systems that are easy to forget in a budget: compressed air with drying, process cooling, exhaust for the flux and lamination fumes, ESD-safe flooring, and the material handling that links the stations. In practice these supporting systems are what separate a list of machines from a working line, and they are the reason a factory should be laid out before it is quoted.
What equipment is needed for solar panels?
The minimum honest list for making a finished, testable module is smaller than people expect: a stringer, a layup and bussing arrangement, a laminator, a framing machine, and testers for EL and IV. Everything else improves throughput, yield or repeatability rather than making the product possible at all. That distinction matters when budgeting, because it separates the stations you cannot start without from the ones you can add as volume justifies them.
What cannot be skipped is testing. A module that has not been EL-tested and IV-tested is an unverified product, and the cost of that verification is trivial compared with the cost of shipping modules with hidden cracks or a misclassified power bin.
What is needed to manufacture solar panels?
Four things, in order of how often they are underestimated: a suitable building, the equipment, the raw-material supply chain, and the people. The building has to carry the load, supply the power and support the lamination and curing temperatures. The equipment is the most visible cost and the most accurately quoted. The supply chain — cells above all, then encapsulant, glass, ribbon and junction boxes — determines whether the line can actually run at its rated capacity.
The people requirement is the quiet one. A fully automatic line still needs process engineers who can read an EL image, diagnose a lamination defect and adjust a soldering profile. Automation removes hands, not judgement, and a factory without that judgement spends its time re-running batches rather than making modules.
Related: Solar Panel Manufacturing Machine: Stations and Layout explains how the same process sequence is re-sized from 5 MW to 1.2 GW and which inputs to freeze before ordering.
Further reading and background data
Public reference material on this topic, published by the organisations that maintain the industry's technology roadmap and market data: