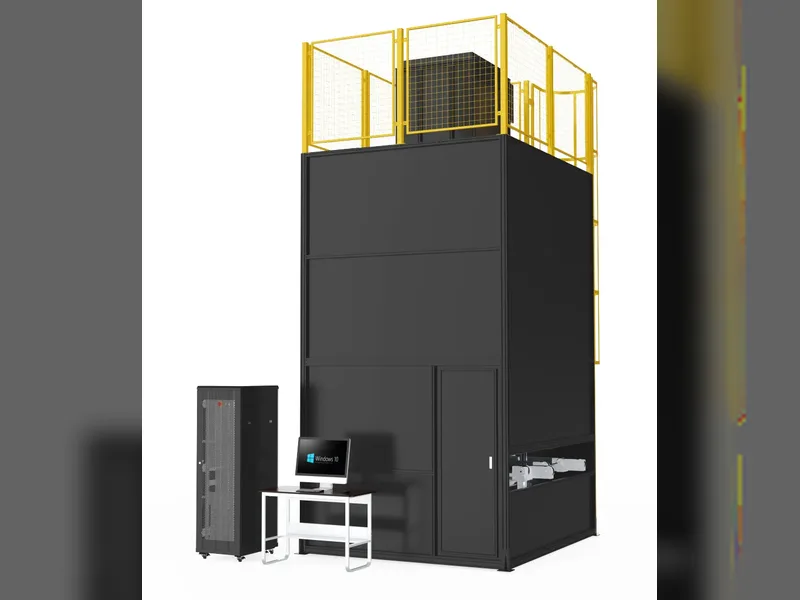
Tabber and Stringer Machine: How It Works, How to Choose
Table of Contents
Tabber and Stringer Machine: How It Works, How to Choose
The one machine every module must pass and no later station can repair — stations, soldering specs, 0BB and BC compatibility, price bands, and the defects that show up in real factories.
PV Module Production · Stringer Selection Guide · by Jerry, Ooitech
One machine decides whether a module holds its power for 25 years: the tabber and stringer machine. Every joint it solders is permanent — no later station can repair a bad one. Here is how the machine works, and how to choose yours.
1. What the Machine Actually Decides
The tabber and stringer solders solar cells together, one by one, through tinned copper ribbon: ribbon bonds to the front grid lines of one cell, wraps to the back of the next, and repeats until a full string exists. Heat melts the ribbon's solder coating into a metallurgical bond with the cell's fingers — and that heating profile, applied to a wafer around 130–180 μm thick, either leaves an intact electrical path or a hidden microcrack.
On the production line the machine sits after cell sorting and before layup, which makes it the first irreversible process between cell and module. Lamination can be re-run, framing can be corrected, but a cold joint or a cracked cell inside a finished string is there forever. That is why experienced buyers spend more time auditing this one machine than the rest of the quotation sheet combined.
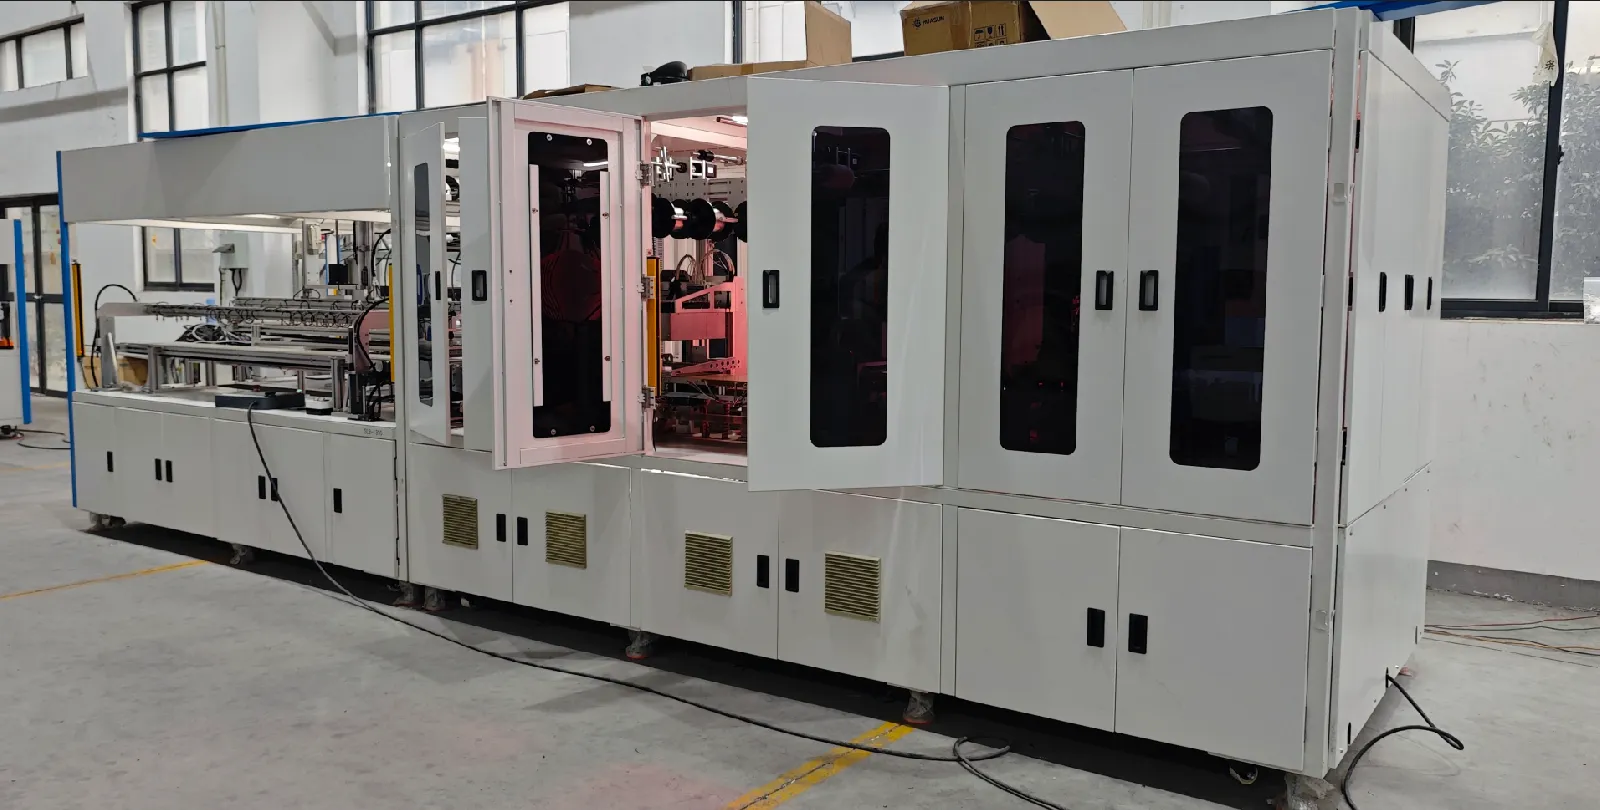
2. Inside the Machine: Six Stations
| Station | What happens | What to check when buying |
|---|---|---|
| 1. Load & sort | Cells loaded, aligned by CCD camera | Alignment precision spec (±0.15 mm class on current machines) |
| 2. Flux spray | Flux prepares the solder surfaces | Dosing consistency; flux is usually sourced locally |
| 3. Ribbon feed | Flat ribbon formed, cut and laid on the pads | Ribbon width range (0.35–1.2 mm typical), cutter adjustability — most alignment defects start here |
| 4. IR tabbing | Infrared lamps reflow the solder | Number of independently controlled heating zones; per-recipe storage |
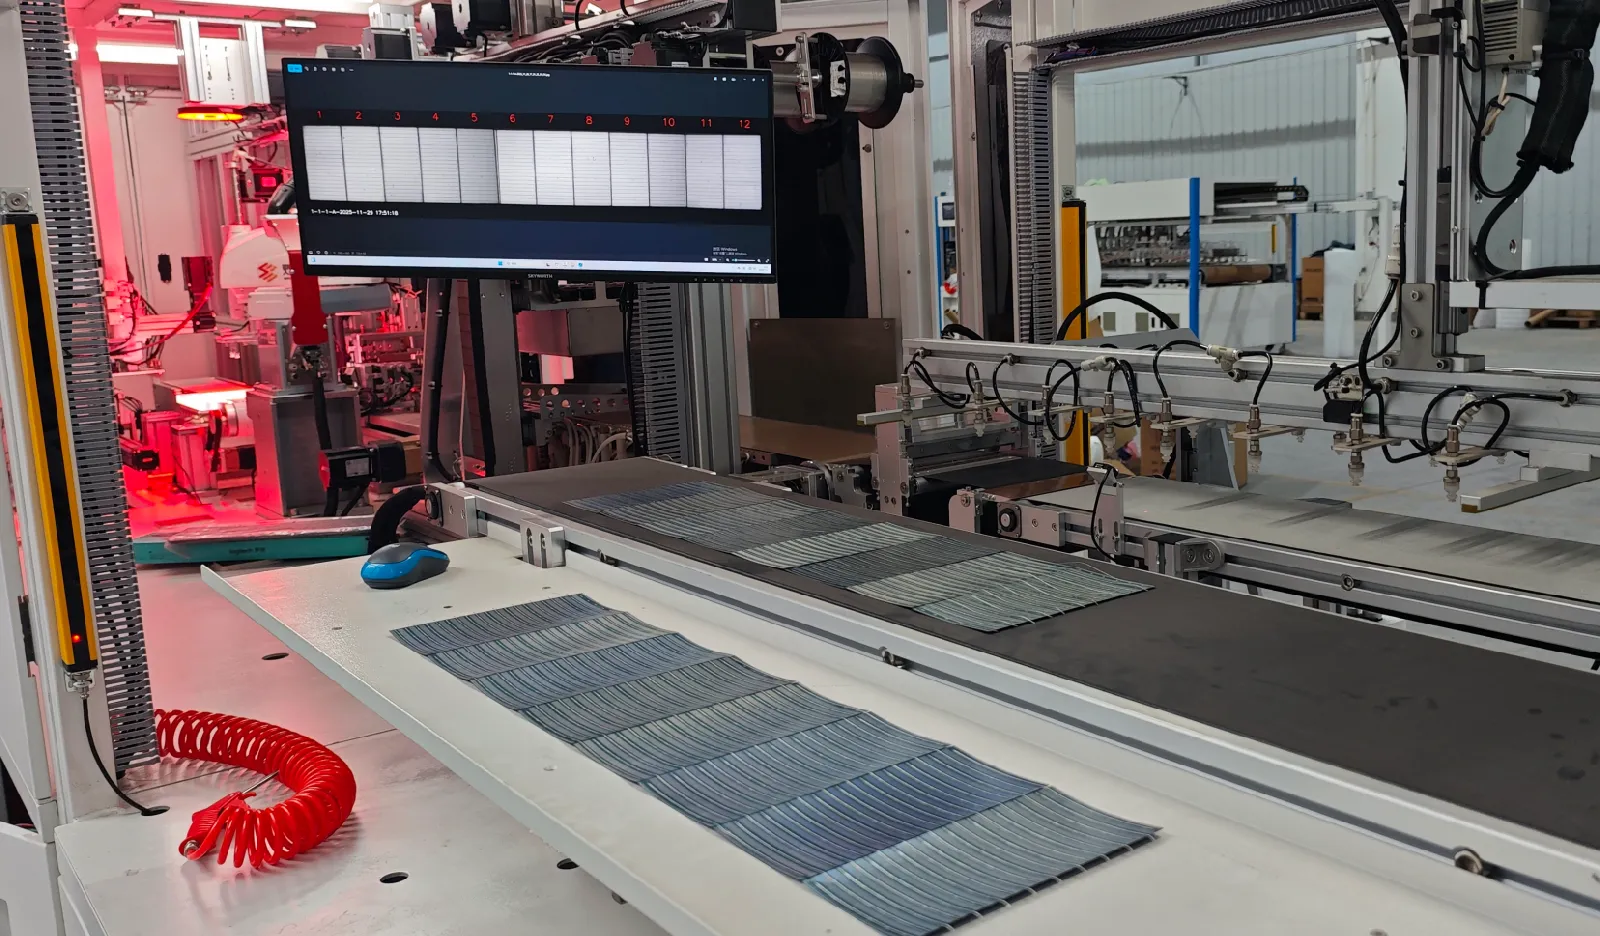
| 5. Stringing | Cells linked front-to-back into the string, robot-stacked | Cell spacing range (1.5–10 mm), handling softness |
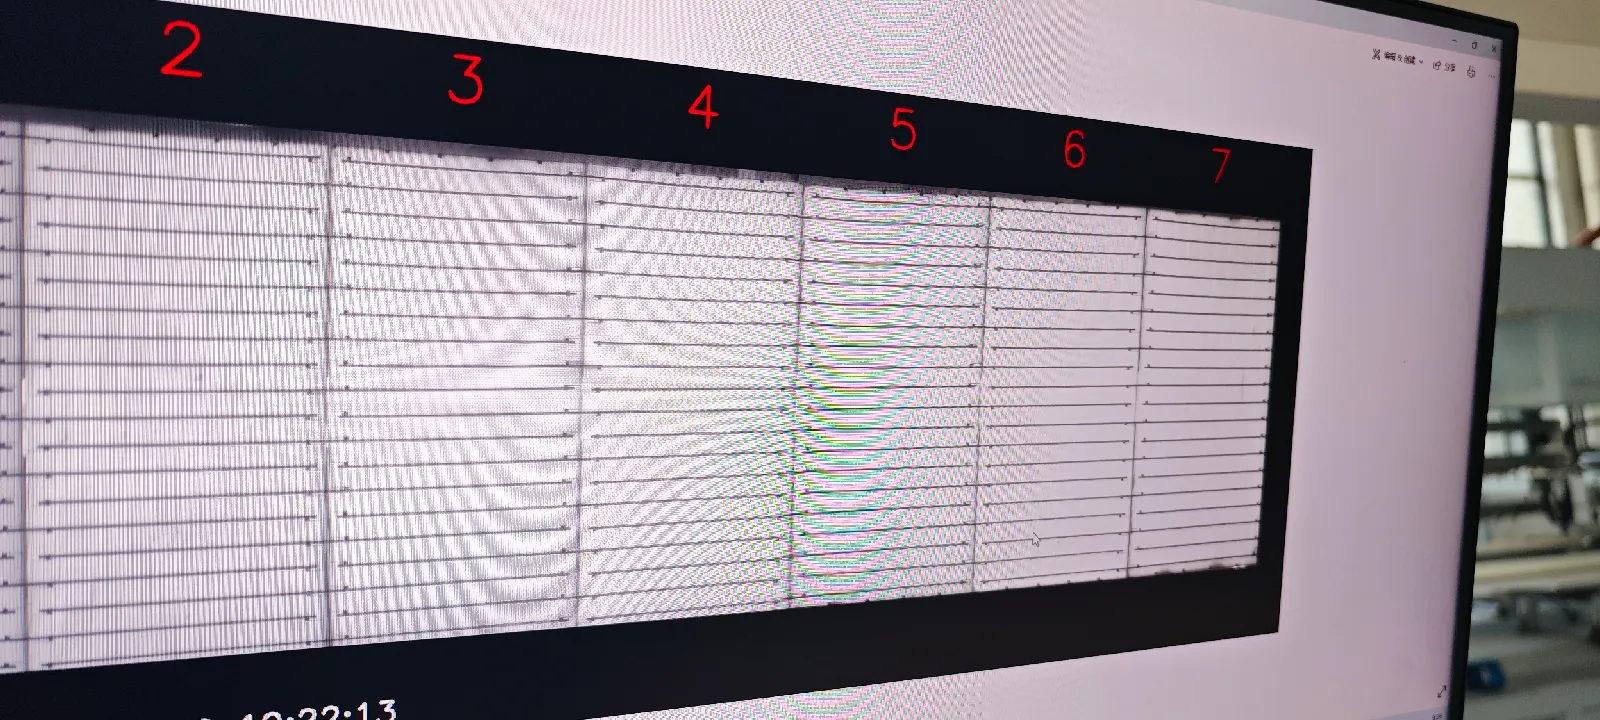
| 6. Inline EL | Electroluminescence check on the finished string | Included or optional; resolution and camera count |
Lines built for zero-busbar (0BB) formats add a seventh station after soldering — glue cure or film lamination — which Section 5 covers. The six-station core is otherwise the same across every manufacturer's machine; what separates quotes is precision, heating control, and how much of the handling is robotic.
3. The Numbers That Matter on the Spec Sheet
Three specifications predict everything else about the machine. Breakage rate: current-generation machines hold ≤0.2% on A-grade cells — accept nothing looser, because breakage at this station is scrap plus rework labor, permanently. Throughput: entry machines run ~1,200 cells per hour, the workhorse class 2,400, and high-speed ATW-class machines 6,800 — size this against your laminator and your shift plan, not against the seller's headline. Positioning accuracy: ±0.15 mm positioning and ±0.2 mm placement are the current standard; as busbar counts rise and fingers get finer, accuracy is what keeps ribbon on pads at speed.
One more spec worth demanding: how many complete cell kits come with the machine, and what a second kit costs. If you plan to run more than one cell format — and most lines eventually do — format changeover lives or dies on spare kits and stored recipes.
4. IR Soldering Won — Confirm It and Move On
Older catalogs list infrared, hot air, laser and induction side by side as if the choice were still open. It is not. Infrared is the mass-production standard — non-contact, mature, with independently zoned temperature control — while hot air has effectively left new lines: uneven heating, slow cycles, and thermal shock that thin wafers cannot take. Laser and induction survive in niche applications at equipment costs the economics rarely justify for module assembly. The decision that actually matters in 2026 is not the heating method but whether the IR platform can upgrade to 0BB later.
5. The Real 2026 Question: Busbar Formats and 0BB
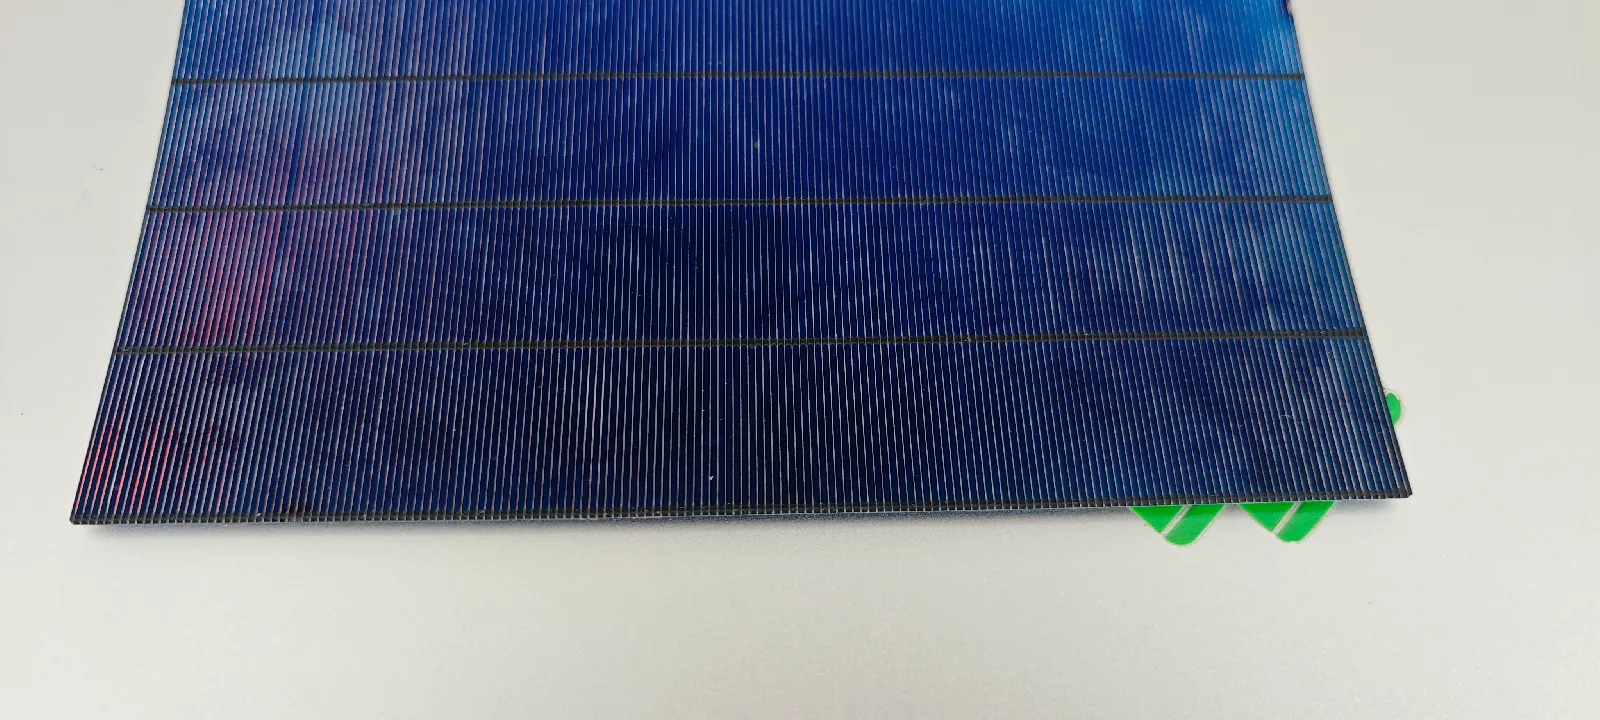
Stringer development over the past five years is one story: busbars from many to none. MBB (multi-busbar) gave way to SMBB (15–25BB), and the industry is now moving to 0BB — fine round wires soldered directly onto the fingers, saving silver paste, cutting shading and raising power. Industry forecasts put 0BB near 90% penetration by 2026, which means a machine bought today that cannot run 0BB risks being outdated within two years. A standard machine covers PERC and TOPCon in 3–20BB natively; 0BB is an add-on process, and the four routes differ enough to change your purchasing:
| 0BB route | How it bonds | Trade-off |
|---|---|---|
| Solder + glue | IR tacks the wire, thermoset glue reinforces | The most economical in mass production; demands high glue-dispensing accuracy — the natural upgrade path for an IR stringer |
| Film | Polymer film holds wires, bonds during lamination | Widest cell-type fit (TOPCon/HJT/BC) and high reliability; film adds cost |
| Glue dispensing | Dispense, route wire, cure | Simple, stable equipment; extra glue cost and possible EL shadow under the wire |
| SmartWire | Composite film + wire grid | Established route; patent-protected until 2034 with high film cost |
6. Cell Compatibility: One Machine, Four Cell Families
| Cell type | Stringing requirement | Mainstream approach |
|---|---|---|
| PERC | Mature, cost-sensitive | Standard IR, MBB/SMBB |
| TOPCon | N-type, SMBB moving to 0BB | Standard IR / 0BB solder+glue |
| HJT | Low-temperature sensitive, thin wafer | Low-temp IR / 0BB film or glue |
| BC (IBC/ABC/HPBC) | Back-contact, no front busbar | BC-compatible stringer configuration — confirm before quoting anything else |
If your business plan includes tolling work — running several customers' cell formats on one line — compatibility is worth more than peak throughput. Quick-change cell kits plus a validated, stored recipe per format let one machine switch between routes in a changeover window measured in minutes; a machine without that flexibility caps your customer list at one technology route.
7. What a Tabber and Stringer Costs, and What Moves the Price
Typical FOB China price bands by machine class: entry machines around $60k–70k, the 2,400-cells/hour workhorse class $120k–140k, and high-speed 6,800-cells/hour ATW-class machines $380k–430k. Within one class, the spread between two quotes usually comes from four items: inline EL included or not (and with how many cameras), robotic versus mechanical cell handling, the number of cell kits and stored recipes included, and how much of the commissioning and training is priced in. When a quote for the "same" class sits 30% below the band, one of those four has quietly left the sheet.
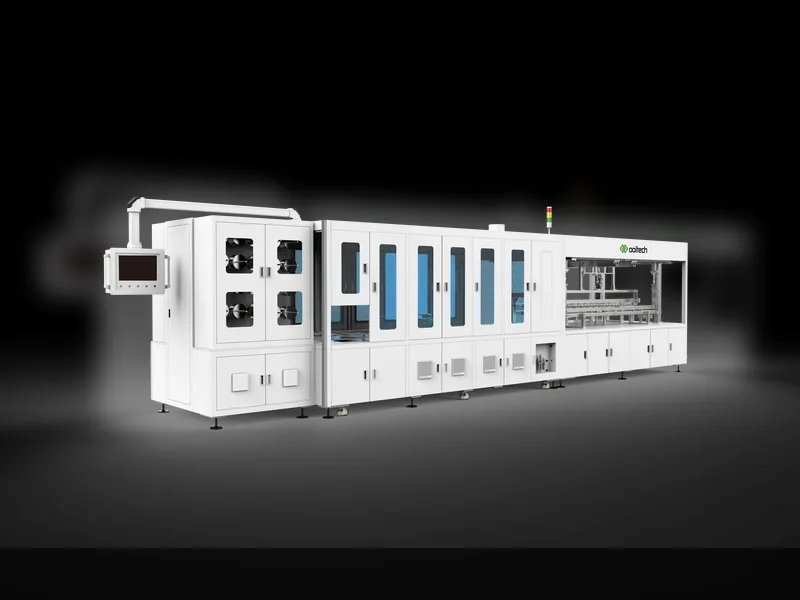
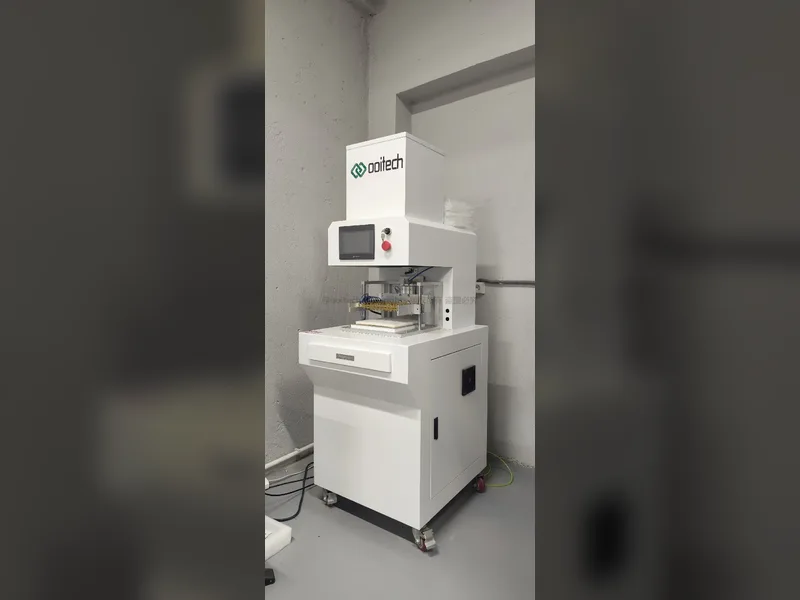
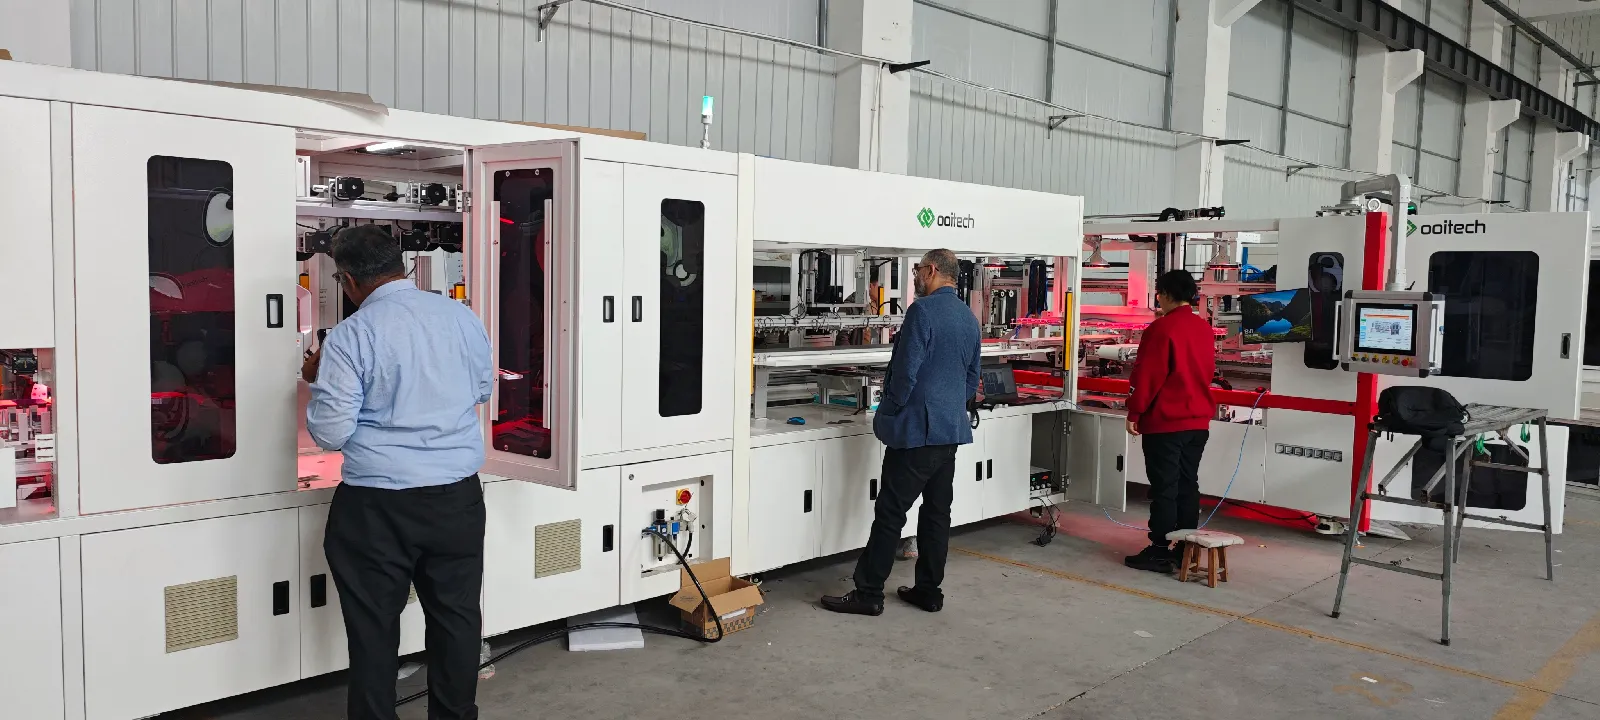
Disclosure, since you will notice anyway: Ooitech sells stringers — our SS-1500B is the entry-class machine, and the SS-2500 is the workhorse in every line we ship. One of ours covers 166–210 mm cells, 3–20BB, ribbon 0.35–1.0 mm wide, with ±0.15 mm positioning, ≤0.2% breakage and three inline EL cameras; BC-compatible configurations and 0BB glue/film upgrades are quoted per project. Use the bands above against any supplier, us included.
8. When Things Drift: Three Defects from Real Factories
Most of the stringer questions that reach our support channel are not hardware failures. They are setup drift, and the same three keep appearing. Wires sitting off the solder pads, usually at the same edge of the string: check the ribbon feed first — rolls seating, ribbon plane level with the cutter, cutter overlap height — before touching temperature. Blackened or unwetted joints at the string edge while the center solders fine: that is a heating-zone profile question, not a cell question; the zone layout needs rebalancing for the format in the machine. Recipe drift after a cell change: every cell format — half-cut TOPCon behaves differently from 182 PERC — wants its own validated heating recipe, and the single most useful habit is storing per-format recipes instead of adjusting one shared setting. Operators who learn that habit in week one stop losing weekends to it in month six.
That is also the honest answer to "how long until we run rated yield": the machine is capable on day one of commissioning; the recipe library and the operator's eye take two to three months to build. Buy the machine from whoever stays reachable for that window.
FAQ — Tabber and Stringer Machine
How much does a tabber and stringer machine cost?
Typical FOB China bands: $60k–70k for an entry machine, $120k–140k for the 2,400-cells/hour workhorse class, $380k–430k for high-speed ATW-class units. Inline EL, robotic handling, spare cell kits and commissioning scope move a quote within its band.
What does a stringer's throughput number actually mean?
Cells per hour, measured on the machine's rated format. Two entry-class stringers at ~1,200 cells/h roughly feed one 16-panel-per-hour semi-automatic line; one 2,400-cells/h machine anchors a 20–60 MW line; 6,800-cells/h machines appear in multiples on 150–600 MW lines. Always check throughput against your laminator's cycle, not in isolation.
Can one stringer run PERC, TOPCon, HJT and BC cells?
PERC and TOPCon, yes, on one standard machine with per-format recipes and cell kits. HJT needs a low-temperature configuration, and BC formats need a BC-compatible stringer. If BC or HJT volume is in your plan, confirm that compatibility before comparing any other specification.
What breakage rate should the spec sheet promise?
≤0.2% on A-grade cells for current-generation machines — the same figure across entry and workhorse classes. Anything looser costs you scrap forever; anything dramatically tighter deserves a verification question about the test conditions.
Why do ribbon wires miss the solder pads?
Almost always ribbon feed setup, not the cell: rolls not seated, the ribbon plane not level with the cutter, or cutter overlap at the wrong height. Fix the feed path first; only then look at heating-zone settings.
Is hot-air stringing still worth considering?
No, for new lines. Uneven heating, slow cycle times and thermal shock on thin wafers have pushed hot air out of mass production. Choose an IR platform and spend the decision time on its 0BB upgrade path instead.
Does the stringer need inline EL?
Yes. Stringing is the first irreversible process, and inline EL is the only check that catches microcracks and misaligned ribbon before lamination locks them inside the module. Skipping it to save cost converts a visible machine price into invisible scrap cost.
What is 0BB and does my machine need it?
Zero busbar: wires soldered directly on the fingers, saving silver paste and cutting shading. Industry forecasts put it near 90% penetration by 2026, so a machine bought today should at least accept a glue or film upgrade later — an IR platform with solder+glue capability is the most natural path.
Specifications reference Ooitech machine data; price bands reflect typical FOB China market ranges and move with configuration — confirm a current quotation before budgeting.